A faster cut is useful only when the part still meets its drawing. Push a tool too hard, and chatter can mark the surface, heat can distort thin stock, and tool wear can quietly shift dimensions. Small changes matter. How to optimize cutting speed without losing precision begins with measuring both outcomes: cycle time and finished-part quality.
McKinsey’s Industry 4.0 research has reported potential manufacturing gains of 10–30% in throughput and 10–20% in quality from digital use cases. These are broad factory-level ranges, not guaranteed results for a single machining operation. Treat them as context, not a speed target. For a more grounded test, ISO 3685:1993 describes tool-life testing for single-point turning tools, underscoring why tool wear belongs in any speed decision. A sharp insert may cut cleanly at one setting, then leave a rough edge after wear builds.
This guide examines seven practical levers: cutting parameters, tool choice, workholding, machine condition, coolant, toolpath, and in-process measurement. Check the chip shape. Listen for chatter. Record the surface finish and tool life. A spreadsheet helps, but it cannot reveal every vibration at the spindle. I would be cautious about treating one successful trial as a proven setting; material batches and setups vary. The aim is a repeatable balance: faster production, stable dimensions, and no hidden quality loss.
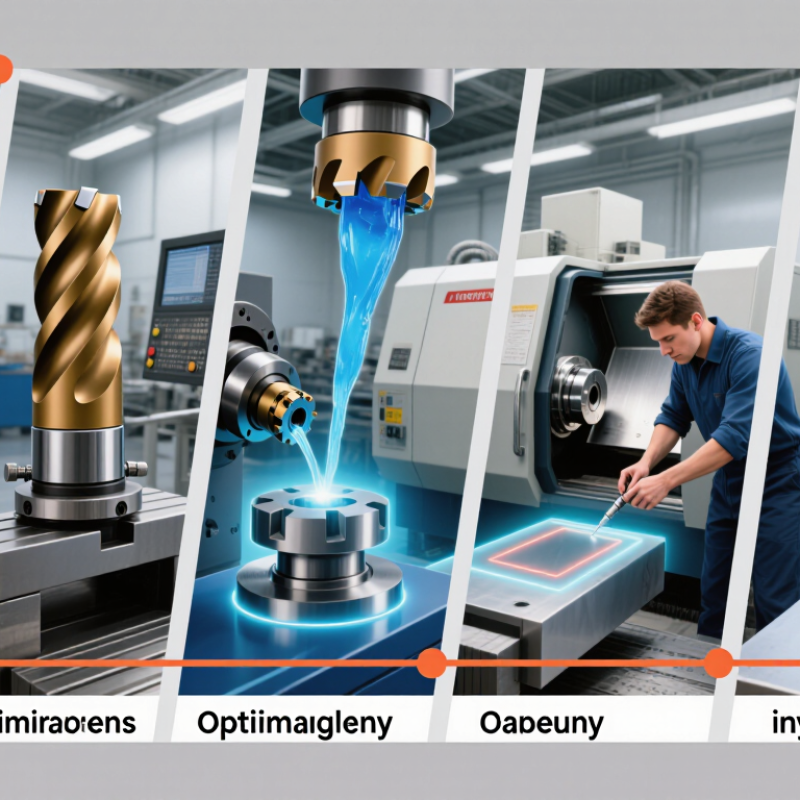
Cutting speed and precision are linked through heat, vibration, and tool behavior. As speed rises, the cutting edge meets the material more often, which can shorten cycle time. But extra heat may soften an edge or expand a workpiece. Even a small change can shift a tight dimension. Faster is not automatically better.
Watch the cut, not just the machine display. A steady sound, clean chips, and an even surface can indicate a stable process, though none proves accuracy alone. Measure a test part with a suitable gauge, then compare its dimensions and finish with the required tolerances. If the edge shows wear or the cut develops chatter, reduce speed or review feed, tool condition, and workholding. Small changes matter.
Material and setup change the relationship. Thin stock may flex under cutting forces; a rigid, well-secured part may tolerate higher speeds. Keep notes on settings and measured results, because repeating a proven setup is more reliable than relying on memory. Still, this is not a neat equation. I would not trust one successful cut as proof that a setting will stay precise through a long run; tool wear and temperature can gradually alter the result. Start with a controlled trial, inspect the part, and adjust one variable at a time.
Choosing the right tool, material, and cutting method often matters more than simply raising spindle speed. Match tool geometry and coating to the workpiece: a sharp, positive-rake insert can reduce cutting forces in softer metals, while tougher edges suit abrasive alloys. Start with the toolmaker’s recommended surface speed, then adjust in small steps. Keep the workpiece firmly supported; even a good tool will chatter on a thin, poorly clamped part. Small details matter.
ISO 3685:1993, an industry tool-life testing standard, uses 0.3 mm average flank wear as a common carbide-tool endpoint under specified turning conditions. Treat this as a test reference, not a universal replacement rule. Choose turning for steady cylindrical cuts, milling for accessible flat or contoured surfaces, and drilling tools suited to hole depth and chip evacuation. One caveat: the ideal setting can still vary between machines, so record actual results.
Tips: Check the material grade, tool condition, and coolant delivery before changing speed. Make one adjustment at a time, then measure the cut with a micrometer or surface-finish gauge. If edges blur or chatter marks appear, back off and inspect the setup. A quick test cut is useful, but it is not always representative of a long production run.
7 Best Ways to Optimize Cutting Speed Without Losing Precision
Feed rate, depth of cut, and machine settings work as a system. Raise feed gradually, not by guesswork. If a 10 mm end mill runs at 6,000 rpm, its cutting speed is about 188 m/min, using the standard cutting-speed formula. That number alone does not prove the cut is safe: material, tool geometry, and engagement matter. Increase feed by 5–10% per trial, then check the edge, chip shape, surface finish, and spindle load. Small steps reveal trouble sooner.
Depth of cut should match tool rigidity and workholding. A long tool extension or thin-walled part may chatter even at modest feed. Reduce radial engagement before making a large speed change; watch for vibration and tapered walls. Keep coolant delivery consistent, confirm tool runout, and check that the workpiece is clamped firmly. ISO 3685:1993 specifies controlled conditions for single-point turning tool-life tests, while ISO 230-2:2014 covers machine-tool axis positioning accuracy and repeatability. These standards offer useful measurement frameworks, not universal cutting settings. Record actual values, including rpm, feed per tooth, depth, and finish. One imperfect habit is trusting a clean first pass too much. Recheck after the machine warms up; thermal drift can change the result.
Cutting faster only works while heat, tool wear, and vibration stay controlled. Ezugwu and Wang’s review in the Journal of Materials Processing Technology reported tool–chip temperatures approaching 1,000°C when machining titanium alloys. That heat can soften the cutting edge and shorten tool life. Use the material supplier’s recommended starting conditions, then raise cutting speed in small steps while checking chip color, edge wear, and surface finish. Keep coolant aimed at the cutting zone; a stream that misses the contact point may add little protection. Small changes matter.
Tool wear needs a measurable limit. ISO 3685:1993 uses average flank wear of 0.3 mm, or maximum wear of 0.6 mm, as common tool-life criteria in specified turning tests. Do not wait for a visibly damaged edge on a precision part. Vibration can leave repeating marks before a tool looks worn, so check tool overhang, workholding, and runout, then compare vibration readings between cuts. A smooth spindle sound is not proof. I would not treat one successful pass as a reliable speed limit; material batches and clamping can change the result. Keep a brief log of speed, wear, vibration, and finish, and adjust one variable at a time.
| Method | Starting adjustment | What to monitor | Precision safeguard |
|---|---|---|---|
| 1. Tune cutting speed in small steps | Change surface speed by about 5–10% per trial, staying within the tool and workpiece material recommendations. | Flank wear, cutting-edge chipping, surface discoloration, and changes in cutting sound. | Compare dimensions and surface finish after each trial; avoid increasing speed if wear or thermal drift rises. |
| 2. Keep feed per tooth or revolution appropriate | Use the tool maker’s recommended chip-load range as a starting point. Adjust feed by roughly 5–10% per test rather than making a large jump. | Chip shape, rubbing, excessive cutting force, edge wear, and spindle load. | Confirm that the tool is cutting rather than rubbing, while checking that feed marks remain within the finish requirement. |
| 3. Reduce engagement when heat or chatter builds | For milling, test a 10–20% reduction in radial or axial engagement, changing one parameter at a time. | Vibration, temperature-related drift, chip evacuation, and cutting load. | Use a consistent tool path and verify feature size and finish after reducing engagement. |
| 4. Improve coolant or lubricant delivery | Direct a steady, suitable coolant or lubricant flow to the cutting zone; use the process-appropriate delivery method and concentration. | Heat at the cutting edge, chip welding, built-up edge, and inconsistent finish. | Keep coolant conditions consistent between finishing passes to limit dimensional changes from temperature variation. |
| 5. Minimize tool overhang and setup flexibility | Use the shortest practical tool extension and secure the workpiece and toolholder firmly. | Chatter marks, deflection, tool movement, and changes in measured dimensions. | Check clearance before shortening the setup, then inspect the part for taper or size error caused by deflection. |
| 6. Check tool runout and tool condition | Measure runout near the cutting edge; where the tooling and process allow, aim for less than 0.01 mm, or follow the tool system’s specified tolerance. | Uneven flute wear, one-sided chip loading, poor finish, and unexpected tool life. | Clean contact surfaces and reseat the tool before measurement; replace damaged or excessively worn tools. |
| 7. Stabilize the machine and verify results | Allow the machine and workpiece to reach a stable operating temperature, then make controlled test cuts and record settings. | Dimensional drift, vibration, spindle load, and repeatability across consecutive parts. | Measure with a calibrated instrument and confirm the result on repeat cuts before adopting the faster setting. |
Note: Adjustment ranges are practical trial increments, not universal cutting parameters. Final settings depend on workpiece material, tool geometry, machine rigidity, and the required tolerance; use the tool supplier’s guidance and validate with inspection cuts.
Speed changes are only useful when the cut remains consistent. Record the starting feed rate, spindle speed, material thickness, and tool condition before adjusting anything. Cut several matching samples, not just one. Measure each part at the same points with calibrated calipers, and note edge quality, burrs, heat marks, and cycle time. Small changes matter. A faster pass may save seconds but leave a rough edge that needs extra finishing.
Keep a simple log for each trial, including the material batch and any setup changes. Compare the results against the part’s tolerance, rather than relying on appearance alone. If dimensions drift or the edge shows excessive heat, reduce speed or check tool wear and clamping. Change one setting at a time; changing feed and speed together makes the cause harder to identify. I have found that rushed measurements can make a good adjustment look like a bad one, so repeat the test after the setup cools. Record every pass. Review the data with the operator, since a faint vibration or changing sound may explain a measurement shift the log cannot.
It can shorten cycle time, but extra heat and vibration may reduce precision. Faster is not automatically better.
Measure a test part with a suitable gauge. Compare its dimensions and surface finish with the required tolerances.
Listen for chatter and inspect the chips and surface. Repeating marks, roughness, or tapered walls may signal trouble.
Increase it in small steps, such as 5–10% per trial. Check chip shape, tool edge, finish, and spindle load. Small steps help.
Thin stock can flex under cutting forces. A rigid, firmly secured part may tolerate higher speeds.
Check tool wear, runout, overhang, coolant direction, and clamping. A coolant stream that misses the cutting zone may offer little protection.
Recheck dimensions after the machine warms up. Temperature changes can expand the workpiece or shift machine alignment.
Record speed, feed, depth, tool wear, vibration, and finish. One clean pass can mislead; conditions may change during a longer run.
How to optimize cutting speed without losing precision begins with understanding the balance between speed, accuracy, and the demands of the material. Select a suitable tool and cutting method, then adjust the feed rate, depth of cut, and machine settings to match the job. Increasing speed alone may reduce accuracy or cause inconsistent results, so changes should be made gradually and with attention to the cut quality.
Precision also depends on managing tool wear, heat, and vibration. Keep tools in good condition, use appropriate cooling when needed, and ensure the workpiece and machine are stable. Measure each result against the required dimensions and finish, then refine the settings based on what you observe. This careful process helps improve cutting efficiency while maintaining reliable, accurate outcomes.
Deepit Cutter